
Related term
Demand Amplification
A tendency observed in multi-step processes, in which the production orders received by each upstream process are more…
View termA production control method in which downstream activities signal their needs to upstream activities.


A production control method in which downstream activities signal their needs to upstream activities. Pull production strives to eliminate overproduction and is one of the three major components of a complete Just-in-Time production system.
In pull production, a downstream operation, whether internal or external, provides information to the upstream operation, usually via kanban cards, about which parts and materials are needed, the quantity needed, and when and where they are needed. Nothing is produced by the supplier process until the downstream customer signals a need. It is the opposite of push production.
There are three basic types of pull production systems:
Supermarket Pull System
This is the most basic and widespread type of pull production, also known as a replenishment system or a type A pull system. In a supermarket pull system, each process has a store, a supermarket, that holds a set quantity of each item it produces. Each process produces only what is needed to replenish what is withdrawn from its supermarket.
Typically, when material is withdrawn from the supermarket by the downstream process, a kanban or some other type of signal is sent upstream to the supplying process, which then replenishes what was withdrawn.
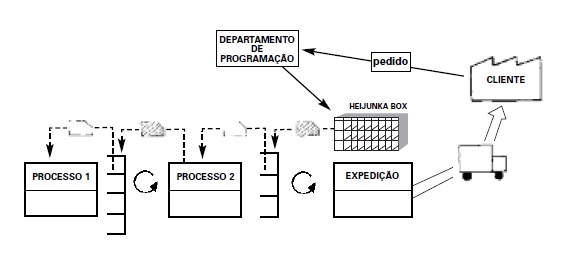
Each process is responsible for replenishing its own supermarket, so daily management of the workplace is relatively simple and kaizen opportunities are relatively easy to see. The drawback of a supermarket system is that a process must hold an inventory of every part it produces, which may be impractical if the variety of parts is very large.
Sequential Pull System
Also known as a type B pull system, the sequential pull system can be used when there is too great a variety of parts to be held in a supermarket. Products are essentially made to order, and overall system inventory is minimized.
In a sequential system, the scheduling department must set the correct mix and quantity of products to be produced. This can be done by placing kanban cards in a heijunka box, usually at the start of each shift. These production instructions are then sent to the initial process in the value stream. This is often done in the form of a "sequential list." Each of the following processes produces, in sequence, the items that reach it from the previous process. FIFO must be maintained continuously for each product.
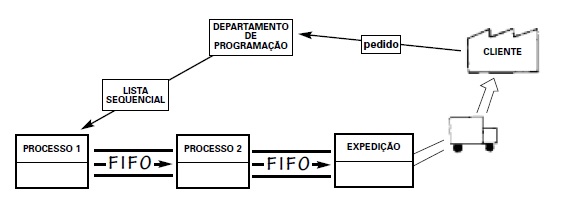
A sequential system creates pressure to keep lead times short and predictable. For this system to work effectively, the pattern of customer orders must be well understood. If orders are difficult to predict, the production lead time must be very short (shorter than the order lead time), or an appropriate supermarket of finished products must be maintained. A sequential system requires strict management to be sustained, and improvements on the shop floor can be more of a challenge.
Mixed Sequential and Supermarket Pull System
Supermarket and sequential pull systems can be used together in a mixed system, also known as a type C pull system. A mixed system may be appropriate when an 80/20 rule applies: a small percentage of the range of parts (perhaps 20%) accounts for most (perhaps 80%) of the daily production volume. An analysis is usually done to segment parts by volume, according to order frequency: (A) high, (B) medium, (C) low, and (D) infrequent.
Type D may represent special orders or service parts. To handle these slow-moving items, a special type D kanban can be created to represent not a specific part but a certain amount of capacity. The production sequence for D products is then set by the method the scheduling department uses for the parts in the sequential pull system.
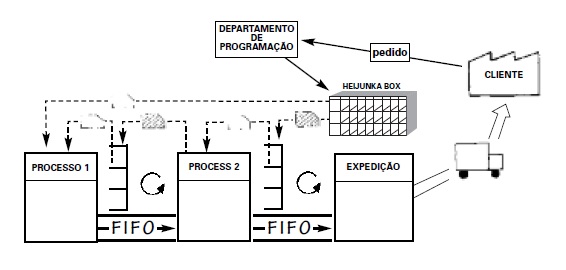
Such a mixed system allows the supermarket and sequential systems to be applied selectively, achieving the benefits of each, even in environments where demand is complex and varied. The two systems can operate at the same time, side by side, horizontally, across an entire value stream, or they can be used for a given part in certain sections of its specific value stream.
A mixed system can make it harder to balance work and to identify abnormal conditions. Conducting and managing kaizen can also become more difficult. Therefore, very rigorous management is needed for a mixed system to work effectively.
Related Article - "Connecting Assembly with Batch Processes via Basic Pull Systems" - Author: Art Smalley - Lean Institute Brasil. Click here to read the full article.
"Connecting Assembly with Batch Processes via Basic Pull Systems Pull systems are a fundamental part of lean manufacturing and are often misunderstood and considered difficult to implement. Specifically, one frequent area of difficulty, I believe, is finding the appropriate connection between assembly line processes and batch processes such as stamping, injection molding, painting, or operations such as machining, for example.
There are three basic types of pull production systems: the supermarket pull system, the sequential pull system, and the mixed pull system, which combines elements of the other two systems. In all three cases, the technical elements that are important for the system to succeed are:
1. Products flowing in small batches (creating "one piece flow" wherever possible).
2. Pulling processes according to takt time (not allowing overproduction).
3. Signaling replenishment through a kanban.
4. Leveling the product mix and quantity
To connect batch processes with the assembly line, the pull production system is used together with a specific type of kanban known as a signal kanban. There are at least three different types of signal kanban, and the appropriate use depends on the nature of your process and of your manufacturing. The three types of signal kanban are:
1. Pattern production kanban
2. Batch-making kanban
3. Triangle kanban
The pattern production kanban establishes a fixed production order and some basic rules on lot size, which may vary somewhat as needed. However, the fundamental pattern, or production order, is always maintained. This creates a fixed production sequence (i.e., a pattern) that is repeated continuously. This style of production is usually necessary in heat treatment, painting, or other processes with specific changeover sequences. While the sequence of products should be fixed in these cases, the actual quantity produced in each cycle is not fixed and varies according to customer needs. This is known as a fixed-order/variable-quantity replenishment cycle.
For example, in an eight-hour cycle, the parts always run from A to F (the difficulty of the changeovers may dictate this order). Central supermarket inventory is a function of the replenishment cycle pattern. Thus, a one-day cycle implies a minimum of one day of inventory that must be held in the supermarket; a one-week cycle means one week of inventory. The main drawback of the pattern production kanban is that the sequence is fixed; you cannot jump from part C to part F.
The pattern production kanban establishes a production rhythm and sequence. As long as the pace of all production is kept close to takt time and the supermarket drives the pull between the two processes, the system works. It is the first, basic step toward establishing production control and a pull system between two processes separated by a supermarket.
The pros are that it creates an established order where none existed before. It also allows the best production sequence to make changeovers easier, if necessary. The cons are that this is not a perfect just-in-time system, since you have to wait your turn in the order as the queue moves along, so some delay is involved. Unfortunately, it also does not tend to pressure the system to reduce changeover times, inventory time, or lead time (except through management intervention).
Batch Control Board
Batch making with a batch control board requires creating a physical kanban for each container of parts in the system. As soon as material is consumed from the supermarket, the kanban is immediately detached and periodically brought back to the preceding batch production process, to a board that lays out all the parts and shows the empty space between each kanban card in the system. This is an example of a fixed-quantity/variable-order style of pull replenishment.
The return of a kanban to the empty space on the board indicates that inventory has been consumed from the supermarket; kanbans not yet returned mean there is still inventory in the supermarket. Once the predefined trigger point is reached, the production operator knows to start making the product to replenish the material in the supermarket. If several trigger points are reached at once, production must set rules on what should be produced first (in this scenario the pattern or sequence is not fixed) and where to produce it. Otherwise, supervisors will decide what to do based on the information available.
This method has several advantages. One is that the scheduling sequence is more flexible than with the pattern production kanban. A second is that it provides a visual representation of inventory consumption and highlights emerging problems in the central supermarket.
There are disadvantages to this type of kanban as well. It requires many kanbans if you have many part types, and the kanbans must be brought back promptly and reliably for the batch control board to be accurate. In addition, there is the inherent problem of several parts reaching the trigger point at the same time. In these circumstances, human judgment is needed to decide what to produce among two or more products that have reached the trigger point. Discipline is required of schedulers and supervisors so as not to allow inventory to build up ahead of when it is needed.
Triangle Kanban
The method Toyota would follow most of the time to link batch processes with the downstream assembly process is called triangle kanban. Below is an example, without much detail, of how to use this method in a lean implementation (see LIB's manual Creating Level Pull for more detailed explanations). The example assumes that you have a batch machining department feeding a final assembly line. The machining department has five machines that make 11 totally different product variations. Demand for each product varies significantly, as does the standard packaging for each part. Setup (changeover) time is roughly three hours."
Explore related terms and go deeper with real-world analyses by our industry leads.
A tendency observed in multi-step processes, in which the production orders received by each upstream process are more…
View term
See how this concept and management mindset were applied in practice to deliver real business results.
Read the full article
Build leadership and problem-solving skills at the gemba with support from our specialists.
See the training
